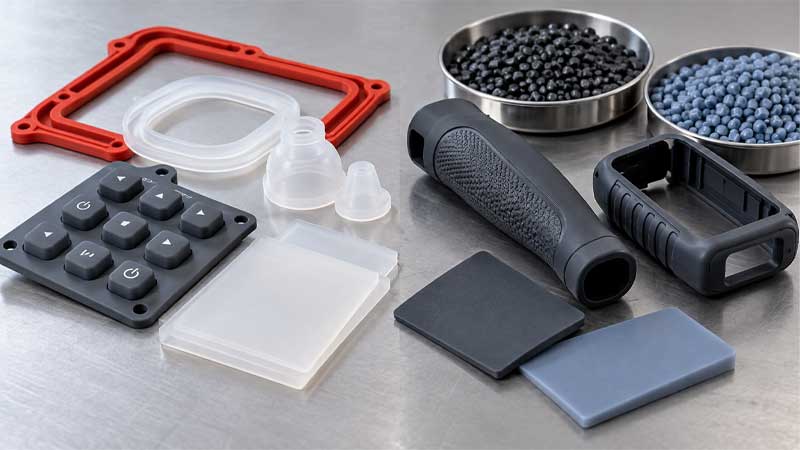
Silicone rubber and thermoplastic elastomers (TPE) are both used for flexible molded components, but their differences become important when a part faces high temperatures, continuous compression, repeated movement, or specific manufacturing requirements.
Silicone generally offers better high-temperature capability and is widely used for molded seals and tactile keypads. TPE provides thermoplastic processing advantages, and certain grades offer excellent abrasion resistance or compatibility with plastic overmolding.
This guide compares their properties, manufacturing methods, costs, and applications to help engineers choose a suitable material.
What Is the Difference Between Silicone and TPE?
The fundamental difference is how the materials respond to heat.
Silicone rubber forms a crosslinked polymer network during curing. This structure maintains its elastomeric form when heated within its operating range, but cured silicone cannot normally be melted and remolded.
TPE combines elastic behavior with thermoplastic processing. It softens when heated and solidifies when cooled, allowing it to be injection molded or extruded using conventional thermoplastic equipment.
This distinction affects operating temperature, tooling, production cycles, and material reprocessing.
What Is Silicone Rubber?
Silicone rubber is based on siloxane polymers with alternating silicon and oxygen atoms in the polymer backbone. Its molecular structure contributes to thermal stability and flexibility across a broad temperature range.
Two common manufacturing forms are high-consistency rubber (HCR) and liquid silicone rubber (LSR). HCR is often compression molded, while LSR is commonly injection molded. Both undergo curing to form the finished elastomer.
Silicone is used in seals, gaskets, electronic keypads, medical components, and flexible connectors. Its limitations include relatively poor resistance to certain fuels and solvents and, for some formulations, lower abrasion resistance than specialized TPU materials.
What Are Thermoplastic Elastomers (TPE)?
TPE is a group of materials that provide rubber-like flexibility without requiring the permanent chemical crosslinking used in conventional silicone rubber.
Major TPE families include styrenic TPEs (TPS), thermoplastic vulcanizates (TPV), and thermoplastic polyurethanes (TPU).
Their properties are not interchangeable. TPU is frequently selected for abrasion-resistant components, while TPV is used in certain sealing applications. Styrenic TPE grades are common in soft-touch grips and consumer product housings.
Many TPE grades can also bond to compatible rigid plastics during overmolding, allowing a flexible grip, sealing lip, or protective surface to be integrated into a housing.
How Do Silicone and TPE Compare in Key Properties?
The following comparison summarizes the differences most relevant to molded component design.
| Property | Silicone Rubber | TPE |
| Polymer structure | Crosslinked during curing | Thermoplastic processing behavior |
| Heat resistance | Some LSR grades rated to 200°C or above | Varies widely; many general-purpose grades have lower limits |
| Low-temperature flexibility | Some grades rated below −50°C | Grade-dependent; some grades perform well at −40°C |
| Compression set | Often favorable for elevated-temperature sealing | Low-compression-set TPV and other grades are available |
| Abrasion resistance | Compound-dependent; may require protective treatment | Abrasion-resistant TPU grades are available |
| Tear strength | Reinforced formulations improve tear resistance | Certain TPU grades offer high tear strength |
| Chemical resistance | Generally good weathering resistance; vulnerable to some fuels and solvents | TPU, TPV, and TPS have different resistance profiles |
| Electrical properties | Many grades provide good insulation | Insulating and conductive formulations exist |
| Reprocessing | Cannot normally be remelted | Many grades can be remelted |
| Manufacturing | Curing is required | Melt processing followed by cooling |
A material’s suitability should be judged by the property that controls component failure, not by the number of advantages listed in a comparison table.
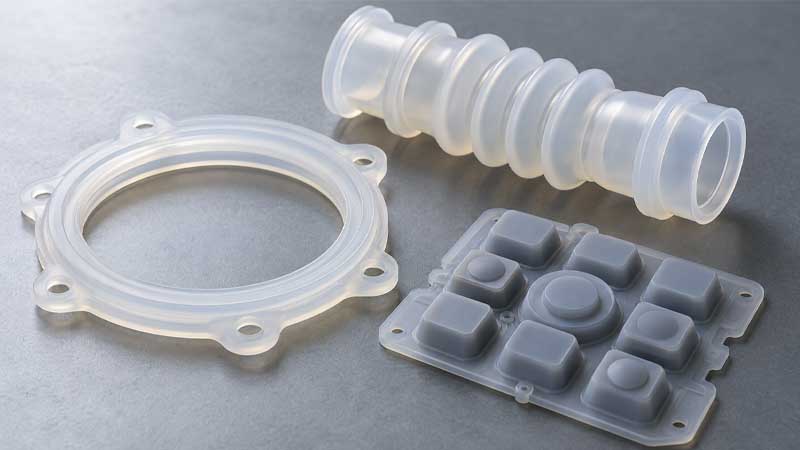
How Do Silicone and TPE Differ in Heat Resistance?
Silicone is generally the stronger starting point for components exposed to sustained high temperatures.
For example, WACKER ELASTOSIL LR 3005/60 A/B liquid silicone rubber has a published operating range of −55°C to +210°C. WACKER recommends adding heat stabilizers for service temperatures above 180°C.
By comparison, KRAIBURG TPE has published a −40°C to +120°C service temperature range for one of its THERMOLAST K FC/CS series, with a maximum of 100°C under dynamic stress.
These examples show an important distinction: the allowable temperature may decrease when a component is subjected to mechanical loading rather than simply exposed to heat.
For a component operating continuously near 180°C, an appropriately rated silicone compound is a practical first candidate. For a soft-touch housing operating below 80°C, high-temperature capability is unlikely to justify silicone by itself.
Engineers should also distinguish operating temperature from molding temperature. A TPE processed at 190°C does not necessarily withstand 190°C during service. Processing temperature indicates how the material is manufactured, not its long-term operating limit.
How Do Flexibility, Compression Set and Durability Compare?
Two materials with the same Shore A hardness may have very different compression recovery, rebound, and fatigue behavior.
Compression set is particularly important for seals and gaskets. When a gasket remains compressed, part of its deformation may become permanent. Excessive compression set can reduce contact pressure against the housing and eventually compromise sealing.
Temperature accelerates this problem for many elastomer formulations.
For example, Covestro Desmopan 9392A GMP TPU reports a compression set of 22% after 72 hours at 23°C. At 70°C for 24 hours, the published values are 56% using ISO 815-1 Method A and 36% using Method C.
These results cannot be treated as a direct temperature comparison because test durations and methods differ. They demonstrate why a compression set number without its test conditions has limited engineering value.
For heated gaskets under sustained compression, appropriately selected silicone is often a useful starting point. Low-compression-set TPE formulations remain candidates when their measured recovery satisfies the sealing requirements.
Repeatedly pressed buttons introduce another failure mechanism. The flexible web experiences cyclic bending, so geometry, stress concentration, and tear resistance influence fatigue life. A material with good compression recovery will not necessarily produce a durable keypad if its web structure is poorly designed.
How Do Silicone and TPE Respond to Chemicals and Weather?
Silicone generally provides strong resistance to UV radiation, ozone, and outdoor weathering. It is useful for exposed controls, sealing components, and equipment subjected to changing environmental conditions.
However, silicone can swell when exposed to certain fuels, oils, and organic solvents. Swelling may change dimensions, hardness, and sealing pressure.
Some TPU formulations provide better resistance to abrasion, oils, or certain solvents, making them suitable for protective surfaces and frequently handled components. Hydrolysis resistance also needs attention when selecting polyester-based TPU for humid or wet environments.
Chemical selection should focus on the fluids the component will actually encounter. For example, a keypad cleaned with alcohol-based solutions requires different compatibility checks from a gasket exposed to lubricating oil.
The key measurements are dimensional change, hardness change, mass change, and retention of the mechanical properties needed for operation.
How Do Silicone and TPE Differ in Manufacturing and Cost?
Material selection affects not only finished-part performance but also the mold, production process, scrap handling, and assembly method.
What Are the Differences Between Silicone and TPE Molding?
TPE is commonly supplied as pellets. During injection molding, it is heated until it flows into the mold, then cooled until the component can be ejected.
LSR normally uses two liquid components that are mixed, injected into a heated mold, and cured. Solid silicone rubber is commonly manufactured through compression molding, although other processes are available.
The important distinction is that TPE solidifies through cooling, while silicone develops its final elastomeric network through curing.
TPE tooling must account for melt flow, cooling, shrinkage, and demolding. Silicone tooling must account for material flow, curing conditions, flash control, and deformation during demolding.
These differences matter when replacing one material with another. A mold developed for a TPE housing or seal may not be suitable for silicone without changes to cavity dimensions, runners, gates, venting, or demolding features.
Material substitution should therefore be reviewed before committing to production tooling.
Is TPE Cheaper Than Silicone?
TPE often provides manufacturing cost advantages when conventional injection molding is suitable for the component.
Suitable TPE processing scrap can sometimes be reused, and certain grades can be overmolded onto rigid plastics. Integrating a soft grip or sealing feature directly into a housing may eliminate separate parts or assembly operations.
Silicone requires curing, and some applications also need secondary operations such as post-curing, printing, coating, or trimming.
However, shorter processing time does not automatically mean a lower finished-part price. Cycle time also depends on mold cavities, cooling requirements, curing speed, geometry, and production automation.
For a simple soft-touch grip, TPE may offer a lower total production cost. For a component exposed to sustained high temperatures or repeated deformation, silicone may avoid performance problems that would otherwise require redesign or replacement.
Cost comparisons should use the expected annual production volume and include tooling amortization, molding cycles, scrap, secondary processing, inspection, and assembly.
Can Silicone and TPE Both Be Recycled?
Many TPE grades can be remelted and reprocessed, making suitable production scrap potentially reusable.
However, repeated processing can change mechanical properties, and bonded multi-material components may be difficult to separate for recycling.
Cured silicone cannot be remelted using conventional thermoplastic processing. Silicone waste can be processed through specialized mechanical or chemical recycling methods, but these require different recovery systems.
Reprocessing manufacturing scrap should not be confused with the practical recyclability of a finished consumer or industrial product.
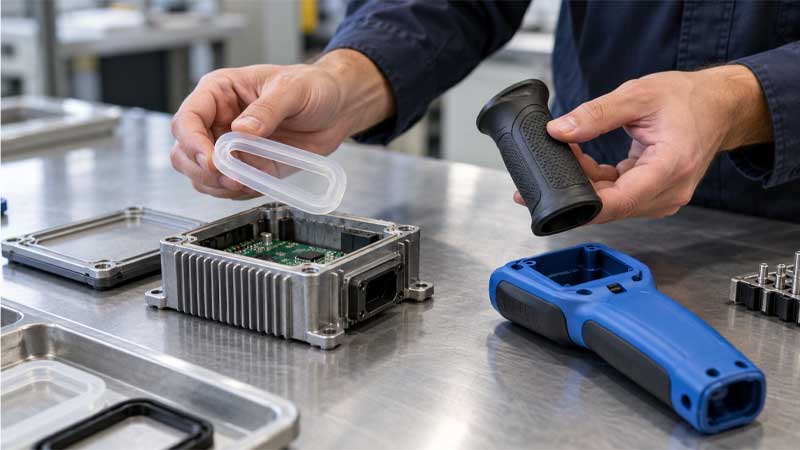
When Should You Choose Silicone or TPE?
The most effective approach is to match the material to the component’s primary performance requirement.
When Is Silicone the Better Choice?
Silicone should be considered first when:
- A component operates continuously at elevated temperatures beyond the rating of available TPE grades.
- A sealing interface requires compression recovery during prolonged heat exposure.
- A molded keypad needs an integral silicone dome with controlled actuation force and tactile feedback.
- The component requires suitable electrical insulation properties.
- Outdoor equipment needs resistance to UV and ozone exposure.
For example, an electronic control keypad exposed to repeated pressing and temperature changes can benefit from a silicone web structure designed for a defined force-displacement response.
For parts exposed to fuels, strong abrasion, or aggressive solvents, silicone should not be assumed to be the best material without examining its specific limitations.
When Is TPE the Better Choice?
TPE is often a stronger candidate when:
- A soft-touch grip must be overmolded onto a compatible plastic housing.
- Abrasion resistance is a primary requirement and a suitable TPU grade is available.
- Conventional thermoplastic processing simplifies production.
- Reprocessing suitable production scrap is important.
- The operating temperature does not require a specialized high-temperature elastomer.
For example, a flexible grip on a handheld device may benefit from TPE overmolding because the soft surface can be integrated with the rigid housing.
The choice of TPE family matters: an abrasion-resistant TPU and a soft styrenic TPE may perform very differently even when their Shore A hardness is similar.
How Do You Choose the Right Material for Your Application?
Start by identifying the requirement most likely to determine component failure.
| Application Requirement | Recommended Starting Point | Reason |
| Continuous operation around 180°C | Appropriately rated silicone | Greater high-temperature capability |
| Soft grip overmolded onto PP | PP-compatible TPE | Potential material bonding and assembly simplification |
| Heated gasket under continuous compression | Silicone or qualified low-compression-set TPE | Compression recovery controls sealing pressure |
| Abrasion-intensive flexible cover | Abrasion-resistant TPU | Strong wear resistance in suitable grades |
| Molded keypad with integral tactile domes | Silicone | Web geometry can produce controlled tactile feedback |
| Indoor soft-touch housing below 80°C | TPE | Thermoplastic processing may reduce manufacturing complexity |
Use the following selection sequence:
- Define the exposure conditions. Record continuous temperature, short-term peaks, chemical contact, and mechanical loading.
- Identify the failure-critical property. For example, compression set for a static seal, abrasion for a protective cover, or fatigue behavior for a keypad.
- Compare specific grades. Check supplier data measured under relevant conditions, including test duration and method.
- Review manufacturing feasibility. Confirm wall thickness, tooling requirements, overmolding compatibility, and production volume.
- Validate the finished component. Test the part in its actual assembly, especially where housing compression, movement, or electrical contact affects performance.
A frequent selection mistake is comparing only Shore A hardness. Hardness measures indentation resistance; it does not establish compression recovery, fatigue life, or suitability for an existing mold.
What Should You Consider When Choosing Silicone for Keypads?
For silicone keypads, material selection must be coordinated with the mechanical structure and electrical interface. A suitable silicone compound alone cannot guarantee consistent button feel or switching reliability.
How Does Material Choice Affect Keypad Tactile Feedback?
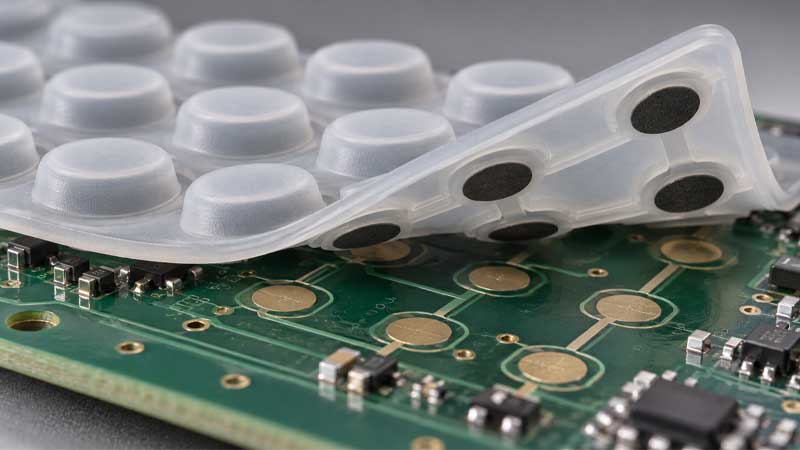
Keypad tactile feedback depends on silicone hardness, web thickness, web angle, dome geometry, and key travel.
Increasing web thickness generally increases the force required to deform the keypad structure. Reducing thickness can lower actuation force but may also affect return behavior and fatigue resistance.
During pressing, a tactile dome reaches a peak force before buckling. The subsequent force reduction creates the snap response felt by the user.
Snap ratio can be expressed as:
Snap Ratio = (Peak Force − Contact Force) / Peak Force × 100%
For example, if the peak force is 200 gf and the contact force is 100 gf, the snap ratio is 50%.
This describes tactile force reduction, not keypad durability. A pronounced snap response still requires sufficient return force and acceptable stress levels during repeated operation.
What Should You Check for Conductive Contacts and Surface Requirements?
Conductive silicone keypads commonly use carbon pills to bridge PCB contact pads when pressed.
Carbon pill diameter, thickness, resistance, and alignment must be considered together with PCB pad geometry and contact pressure. Increasing pill diameter may improve available contact area but can create clearance problems between neighboring conductive pads.
Printed legends, laser-etched backlighting areas, and protective coatings also require appropriate surface design. Abrasion and cleaning exposure can affect graphic durability even when the underlying silicone remains functional.
For related designs, see SKF’s Conductive Silicone Keypads and Tactile Silicone Keypads.
How Should You Validate Silicone Keypad Material Performance?
Validation should focus on measurable operating requirements rather than material hardness alone.
For tactile and conductive keypads, relevant tests include actuation force, key travel, snap ratio, contact resistance, operating cycles, graphic abrasion, and coating adhesion.
PCB alignment and housing assembly should also be checked. Where sealing is required, the complete housing and keypad assembly must be evaluated because a silicone keypad alone does not establish an IP protection rating.
Frequently Asked Questions About Silicone vs TPE
Is TPE the Same as Silicone?
No. Silicone forms a crosslinked elastomer during curing, while TPE retains thermoplastic processing behavior. The materials differ in polymer structure, molding methods, and thermal performance.
Which Is More Heat Resistant, Silicone or TPE?
Silicone generally has the advantage for sustained high-temperature applications. Some commercial LSR grades are rated above 200°C, while many general-purpose TPE materials have lower operating limits. Specific grades must be compared using their published service temperature ratings.
Is TPE Cheaper Than Silicone?
TPE can be less expensive when thermoplastic injection molding, suitable scrap reuse, or overmolding reduces production costs. Silicone may justify higher processing costs when its performance is required for the component’s service conditions.
Can TPE Replace Silicone in a Product?
Yes, when a suitable TPE satisfies the required temperature, mechanical, chemical, and dimensional performance. Replacement may still require tooling changes because the materials use different processing methods.
Conclusion
Silicone generally offers advantages for high-temperature components, elastic sealing structures, and molded tactile keypads. TPE provides thermoplastic processing benefits, while selected TPU and TPV grades can offer strong abrasion resistance or suitable compression recovery.
The most useful comparison focuses on the property’s role in component performance: temperature capability for heated parts, compression recovery for seals, abrasion resistance for protective covers, and tactile response for keypads.
For custom silicone keypads, SKF can review material selection alongside actuation force, web geometry, conductive contacts, and manufacturing requirements. Share your drawings, PCB layout, operating conditions, and expected production volume to discuss your design.