A Liquid Silicone Rubber (LSR) keypad is a high-performance component made from a flexible elastomer known as liquid silicone. LSR keypads are produced using Liquid Injection Molding (LIM), a precise and efficient method that ensures consistent quality and performance across mass-production runs. These keypads are designed to meet the demands of various industries, offering durability, flexibility, and excellent tactile feedback.
For a complete breakdown of silicone keypad design, check out our comprehensive [silicone rubber keypad design guide].
What Is a Liquid Silicone Rubber Keypad?
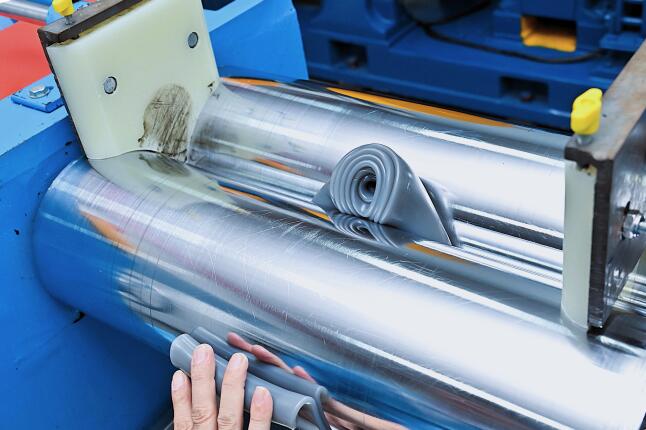
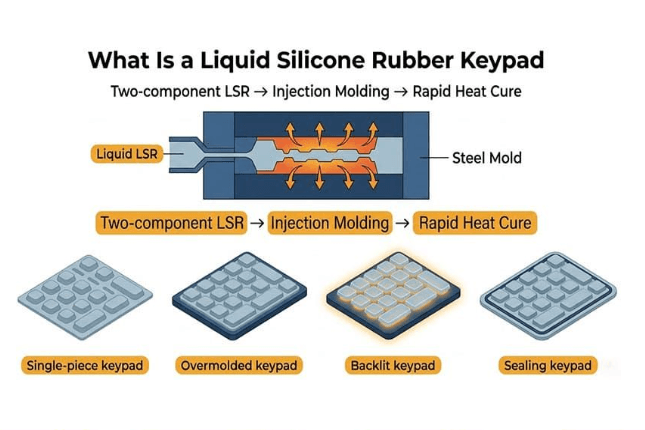
A liquid silicone rubber keypad is a silicone rubber keyboard or button pad produced from two‑component liquid silicone by injection molding rather than traditional solid silicone compression molding.
LSR is pumped in liquid form into a closed mold where it cures rapidly under heat. This process makes LSR keypads especially suitable for precision, repeatability, and automation in modern devices.
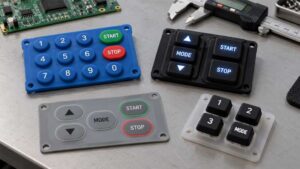
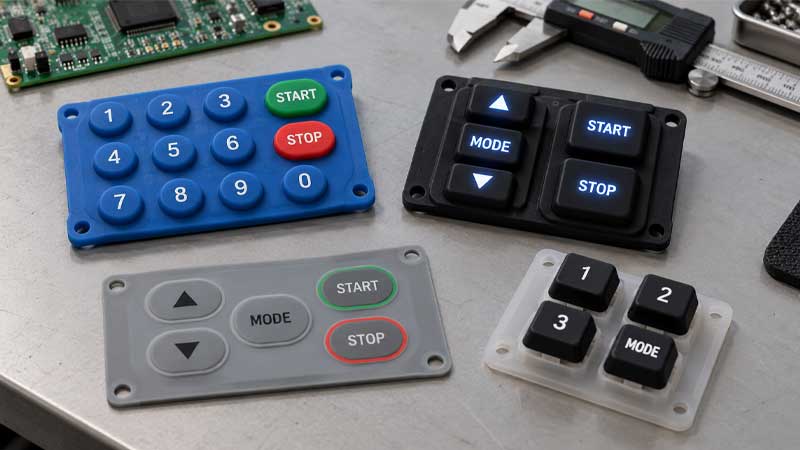
Typical LSR keypad structures include the following:
- Single‑piece silicone rubber keypads
- Keypads overmolded to plastic frames or PCB carriers
- Backlit keypads with translucent or clear windows
- Sealing keypads that combine keys and gaskets in one part
Key Material Properties of LSR Keypads
Superior Mechanical Performance
LSR keypads are known for:
- High tear strength, which resists cracks around thin webbing and domes.
- Excellent rebound and elastic recovery, maintaining crisp tactile feel over millions of actuations.
- Low compression set, so keys recover after long‑term pressing or static load.
This makes LSR ideal for keypads in demanding environments where long lifetime and stable click feeling are mandatory.
Wide Hardness Range for Design Freedom
LSR materials are available across a broad hardness range, typically from about Shore A 5–90.
For keypads, commonly used hardness ranges are:
- Soft tactile keys: 30–40 Shore A
- Standard keys: 50–60 Shore A
- Stiffer industrial or sealed keys: 60–70 Shore A
This flexibility allows you to fine‑tune actuation force, key travel, and snap ratio for each application while keeping the same basic material system.
Transparency and Backlighting Capability
Many LSR grades offer excellent transparency or high translucency.
This is particularly valuable for:
- Backlit keypads and illuminated icons
- Indicator windows integrated into the keypad
- Light-pipe style features inside the silicone mat
Designers can mix opaque and translucent sections or use printing and laser etching to create sharp backlit legends while maintaining robust mechanical performance.
Environmental & Chemical Resistance
LSR keypads typically show the following:
- Stable performance over wide temperature ranges (from low sub‑zero to high operating temperatures)
- Resistance to water and moisture
- Good resistance to weathering, UV, and yellowing
- Good resistance to many oils and chemicals, depending on grade
This combination makes LSR keypads suitable for automotive, outdoor instruments, medical devices, and industrial control panels.
LSR Keypad vs. Compression-Molded Silicone Keypad
Comparison
Both materials feel similar in your hand. The differences are in production consistency, long-term performance, and total cost of ownership. You can find more information about the differences between LSR and HCR keypads here.
| Dimension | LSR Injection Molding | Compression Molding (HCR) |
|---|---|---|
| Tooling type | Precision hardened steel, hot runner | Steel or aluminum, open mold |
| Tooling cost | Higher | Lower |
| Per-unit cost at 10,000 pcs | Lower | Higher (labor-intensive) |
| Cycle time | 15–45 seconds | 3–8 minutes |
| Parting line | Near invisible | Visible |
| Flash | Essentially none | Present — needs removal |
| Dimensional tolerance | ±0.02–0.05 mm | ±0.1–0.2 mm |
| Batch consistency | Very high (automated) | Moderate (manual-dependent) |
| Service life | 5 million+ actuations | Under 3 million |
| Backlit performance | Excellent | Poor |
| Certification suitability | FDA, IATF, USP, UL | Limited options |
When to Choose LSR — and When Compression Molding Still Works
Choose LSR injection molding when:
- Production volume exceeds 5,000 pcs per year
- The product requires tight dimensional tolerances (e.g., backlighting, fine key geometry)
- Keys will be backlit or have laser-etched legends
- The application requires medical, automotive, or food-grade certification.
- Consistency across hundreds of thousands of units is mandatory.
- The product will face UV exposure, chemical contact, or wide temperature swings.
Compression molding still works when:
- Volume is under 2,000 pcs per year, and tooling budget is constrained
- Key geometry is simple and tolerances are wide.
- No certification requirement beyond basic RoHS
- The product is in early-stage development, and geometry may change.
- Delivery speed is prioritized over cosmetic perfection.
A note on total cost: Many buyers choose compression molding because the mold is cheaper. This is correct for low-volume situations. But for anything above ~5,000 pcs per year, the math usually reverses—LSR’s faster cycle time, near-zero scrap rate, and elimination of de-flashing labor make the total cost lower over the product’s lifetime.
LSR vs. RTV Silicone — Which Is Right for Your Project?
Material Differences at a Glance
RTV (Room-Temperature Vulcanizing) silicone is frequently mentioned alongside LSR, especially in prototyping conversations. They are both silicone. But they serve completely different purposes.
| Dimension | LSR | RTV Silicone |
|---|---|---|
| Cure mechanism | Platinum addition cure, heat-activated | Moisture cure (1-part) or addition cure (2-part), room temperature |
| Cure time | 15–45 seconds in mold | 2–24 hours at room temperature |
| Hardness consistency | Excellent — stable across batches | Variable — sensitive to mix ratio and humidity |
| Mechanical strength | High tensile and tear strength | Moderate — varies widely by grade |
| Long-term durability | Rated for millions of cycles | Suitable for low-cycle or short-term use |
| Tooling requirement | Precision steel mold required | Works with soft molds, silicone molds, or no mold |
| Tooling cost | High | Low to negligible |
| Per-unit cost at volume | Low | High — labor-intensive process |
| Automation capability | Fully automatable | Mostly manual |
| Color matching at scale | Consistent | Suitable for single-unit color tests |
The 5-Step Decision Process
Use this framework to decide which material and process is right at each stage of your project.
Step 1 — Identify your project phase. Design validation? Use RTV. Production? Plan for LSR from the start.
Step 2 — Estimate your annual volume.
- Under 2,000 pcs/year → RTV or compression molding keeps tooling investment manageable.
- Over 5,000 pcs/year → LSR injection tooling pays back quickly through lower unit cost and scrap.
- Between 2,000–5,000 pcs → Calculate lifetime cost both ways. LSR often wins after year two.
Step 3 — Assess certification requirements. Automotive, medical, or military applications almost always require LSR. The material traceability, purity, and process control of LIM are prerequisites for IATF 16949, FDA, or MIL-SPEC compliance. RTV and basic compression silicone cannot reliably meet these standards at scale.
Step 4 — Calculate total lifecycle cost. Do not compare mold cost alone. Include the following: tooling amortization, per-unit material cost, de-flashing labor, scrap rate, rework, and time-to-market impact. Over a 3-year horizon, LSR is almost always cheaper above 5,000 pcs/year.
Step 5—Validate feel with prototypes before cutting steel. This is the most important practical step. Lock in your snap ratio, actuation force, and key travel using RTV samples. Optimize the dome geometry. Only then commit to the LSR steel mold. This workflow prevents the most common and most expensive mistake in keypad development: modifying a steel mold because the tactile feel was wrong.
Keypad Tactile Feel: How Shore A Hardness and Snap Ratio Work Together
Shore A Hardness
Shore A hardness is the single most impactful material parameter for keypad feel. Choose wrong, and users will struggle to press (too hard) or bottom out with no feedback (too soft). Neither is acceptable in a finished product.
| Shore A Range | Tactile Character | Typical Applications |
|---|---|---|
| 10–20A | Extremely soft, pillow-like | Medical wearables, infant devices, accessibility aids |
| 25–35A | Soft, light snap | Remote controls, smart home devices, consumer electronics |
| 40–50A | Medium — clear click, fast return | Automotive controls, industrial panels, gaming peripherals |
| 55–65A | Firm, positive feedback | Military, outdoor, waterproof enclosures |
| 70–80A | Hard, minimal travel | Structural buttons, combined keypad/seal components |
Practical rule:
- For keypads pressed lightly with fingertips (remote controls, consumer devices): 30–40A
- For keypads pressed firmly or with gloves (industrial, automotive): 45–60A
- For structural or sealing applications where minimal flex is desired: 65–80A
Snap Ratio
The snap ratio is the percentage drop from actuation force peak to holding force after the dome collapses.
A typical target snap ratio for a pleasant “click” feeling is roughly 40–60%, depending on application and user preference.
- Too low snap ratio → keys feel mushy, no clear click.
- Too high snap ratio → keys may feel harsh or unstable, especially for non‑technical users.
To control snap ratio, you can adjust the following:
- Dome height and shape.
- Web thickness and transitions.
- Shore A hardness of the LSR material.
LSR Keypad Manufacturing Process
Step-by-Step LIM Process
- Requirement definition Confirm key layout, actuation force, travel, backlighting, sealing level, and expected volume.
- Design & 3D modeling Create 3D CAD of the liquid silicone rubber keypad, including domes, webbing, and integrated seals.
- Mold design Design the steel mold with proper parting lines, gating, cold runner or needle valves, and vents tailored for LSR flow.
- Tool manufacturing Machine and finish the mold cavities, runners, and venting features, then assemble and test the mold.
- LIM setup: Install the mold in the injection machine, connect the LSR dosing unit, and set temperature, pressure, and timing parameters.
- Trial production Run trials; fine‑tune process conditions; and verify dimensions, tactile feel, and surface quality of sample keypads.
- Mass production & quality control Start stable production with defined process windows and perform regular inspection on critical dimensions and performance metrics.
Mold Design Critical Points for Keypads
- Thin web and dome areas need excellent venting to avoid air traps and burn marks.
- Gate locations must support uniform filling and avoid weld lines in functional or cosmetic zones.
- Parting line design should minimize visible marks and avoid cutting across critical sealing or tactile areas.
- Ejection must protect delicate domes; often vacuum or air‑assist ejection is preferred over aggressive ejector pins.
Secondary Finishing Options
| Finishing Option | Purpose | Common Use Cases |
|---|---|---|
| Screen printing | Add legends, logos, simple graphics | Non‑backlit keys, branding |
| Spray coating | Change surface feel, color, or gloss | Soft‑touch feel, wear‑resistant surface |
| Laser etching | Create backlit legends by removing paint | Backlit keys with icons and text |
| Epoxy / PU top coating | Enhance abrasion resistance, gloss | High‑wear keys, premium appearance |
| Pad printing | Small multi‑color icons | Compact symbols, decorative details |
Applications of LSR Keypads
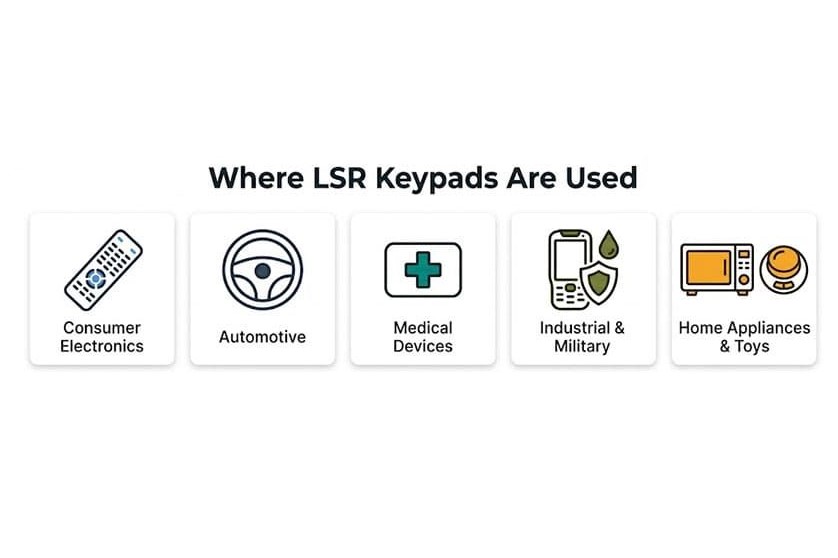
Consumer Electronics
Liquid silicone rubber keypads are widely used in remote controls, set‑top boxes, gaming controllers, and handheld devices.
Designers value the slim structure, comfortable touch, and support for backlighting and branding.
Automotive
In automotive interiors, LSR keypads appear in steering‑wheel buttons, HVAC controls, multimedia panels, and keyless entry pads.
They must endure vibration, temperature cycling, UV exposure, and high actuation counts over many years.
Medical Devices
Medical keypads need easy cleaning, chemical resistance, and reliable operation.
LSR keypads are used in diagnostic equipment, infusion pumps, and control panels where a sealed and hygienic user interface is critical.
Industrial & Military
Industrial and military devices need robust keypads that work under shock, dust, moisture, and sometimes extreme temperatures.
LSR keypads can integrate sealing and rugged domes, making them suitable for portable radios, field instruments, and rugged controllers.
Home Appliances & Toys
In home appliances, LSR keypads appear on microwave ovens, washing machines, ovens, and smart home devices. For toys and kids’ electronics, soft and safe silicone surfaces with vivid colors improve user experience and safety.
Customization Options for LSR Keypads
Material & Hardness
You can choose different LSR grades based on:
- Shore A hardness.
- Color and translucency.
- Special requirements, such as improved flame resistance, low volatility, or specific regulatory compliance.
Color & Appearance
Customization options include:
- Solid colors, translucent colors, and clear windows.
- Matte, semi‑gloss, or glossy surface textures.
- Combined colored zones on one keypad for visual grouping or branding.
Legend & Marking Methods
| Method | Pros | Cons / Notes |
|---|---|---|
| Screen printing | Cost‑effective, flexible design | Wear risk if not protected |
| Pad printing | Good for small detailed icons | Limited coverage area per stamp |
| Laser etching | Perfect for backlit keys | Requires coating layer over base silicone |
| Molded‑in marks | Very durable, no extra process | Limited resolution, not ideal for fine text |
| Epoxy labeling | Premium look, thick gloss surface | Extra cost and process complexity |
Conductive Contact Options
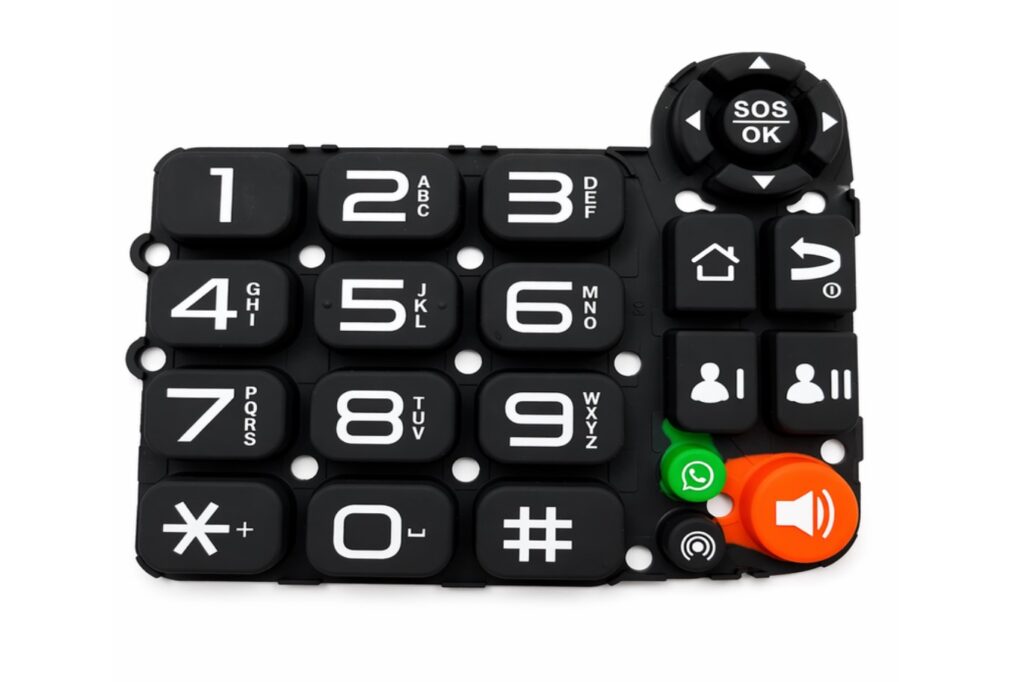
LSR keypads usually actuate a circuit via a conductive element on the underside of the key:
- Carbon pills for standard low‑current contact.
- Gold‑plated metal domes combined with LSR overlay for extremely crisp tactile and low contact resistance.
- Conductive silicone pads where integrated conductive rubber is preferred.
The choice depends on circuit type, required contact resistance, lifetime, and budget.
Why Choose SKF Silicone
As a China-based silicone manufacturer with over 14 years in the silicone industry and international projects, SKF focuses on:
- Professional support for liquid silicone rubber keypad design, from concept to mass production.
- In‑house engineering for mold design, hardness selection, and tactile optimization.
- Stable LSR material supply, consistent color and hardness control, and reliable delivery for long‑term programs.
FAQs
Is the LSR keypad safe for body contact?
Yes. LSR keypads are safe for body contact as they are non-toxic and can be FDA-certified for medical and food-grade applications.
What curing agent is used for liquid silicone rubber keypads?
The curing agent used for LSR keypads is typically a platinum-based catalyst, which ensures fast and precise curing.
Can I get a small batch of LSR keypads without committing to expensive steel tooling?
Yes. Soft aluminum rapid tooling or RTV cast samples allow geometry and tactile validation from as little as 1 piece before any steel mold investment is made.
Do LSR keypads require a separate gasket for waterproofing?
LSR keypads do not always require a separate gasket for waterproofing, as they can be molded with integrated sealing features for waterproof performance.
How long is the lifespan of an LSR silicone keypad?
Typically 5~10 million actuations. But it depends on dome geometry design or conductive carbon pill, hardness of silicone material, and environmental conditions in actual use.
Conclusion
Liquid silicone rubber (LSR) keypads play a significant role in modern interfaces, which make a balance between soft tactile response and high durability. Compared to conventional compression molding, liquid injection molding (LIM) within LSR offers a solution that requires specific scale, consistency, high precision, and enhanced mechanical strength. At the same time, although a relatively high investment in tooling lies there, benefits for the long term are a more cost-effective option for your silicone keypad project, including rapid cycle time and exceeded lifespan.
More information about the requirements for your project will be sent to our SKF engineers’ team, and we’ll offer professional help.